Screws
We manufacture new feedscrews and refurbish worn ones for the plastics, rubber and feed industries. We cover extrusion, injection moulding, blown moulding, compounding and recycling.
Manufacture
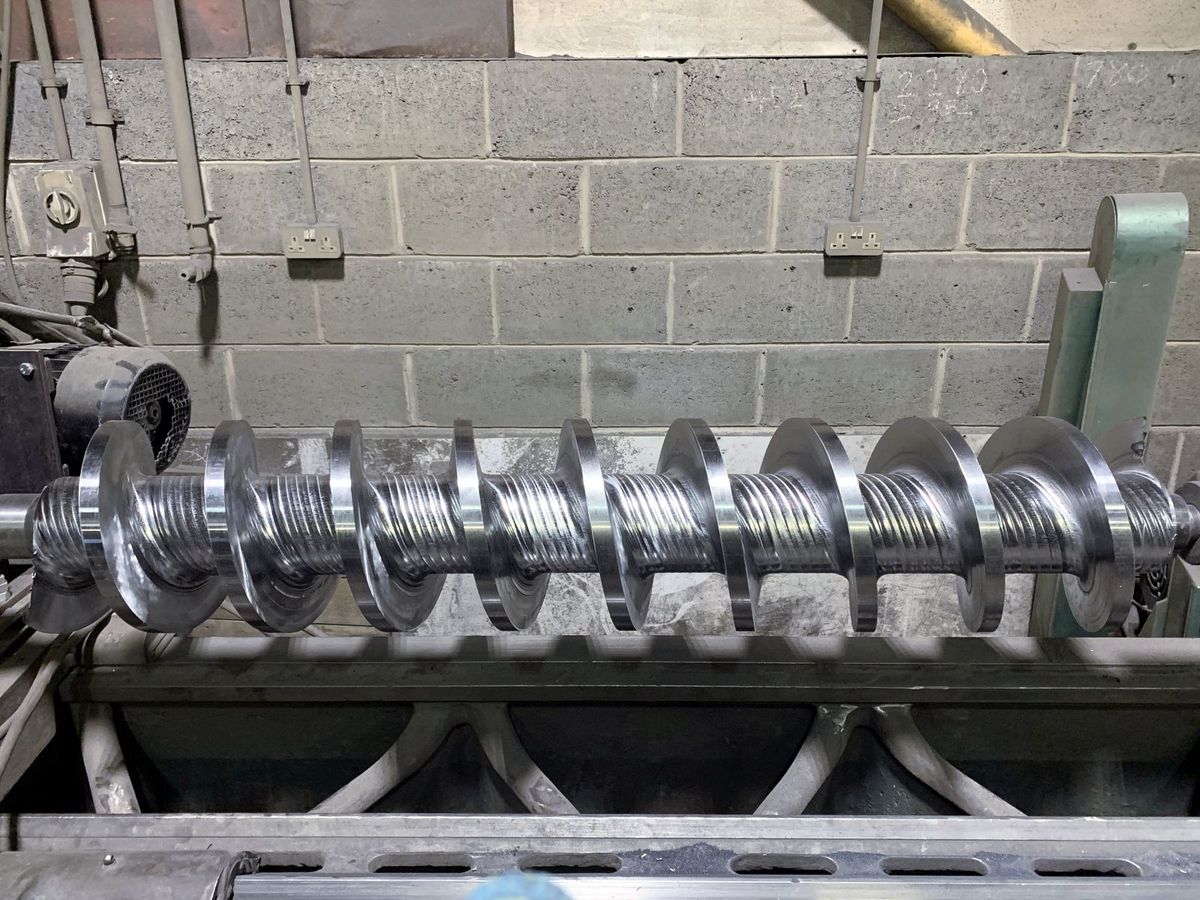
We manufacture new screws as direct replacements for your OEM part. Our standard screws are machined from EN41B (905M39) nitriding steel, then nitrided for more than 80 hours. For high-wear work, we hard-face the flight tips with Stellite or Colmonoy to produce a bimetallic screw. We also offer hard chrome plating, Armoloy and tungsten carbide coatings. We’ve manufactured screws for machines including Battenfeld, Boston Matthews, Plasmac and S&B.
No drawing? We can make one in any of three ways:
| New screws | 20–180 mm diameter, any length |
|---|---|
| Refurbishment | 50–450 mm diameter, up to 6200 mm long |

Refurbishment
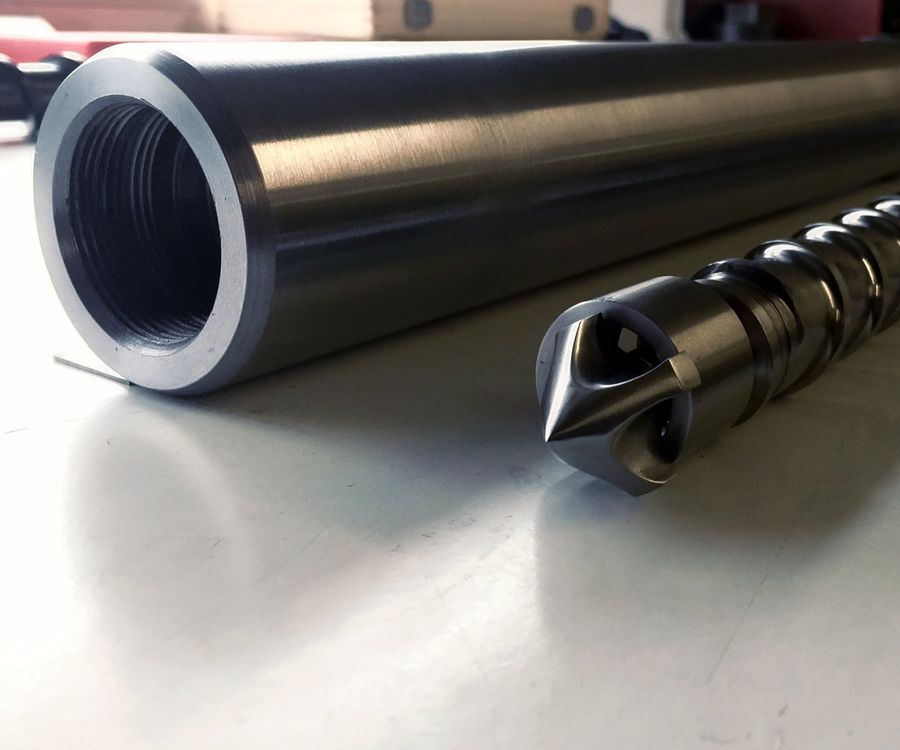
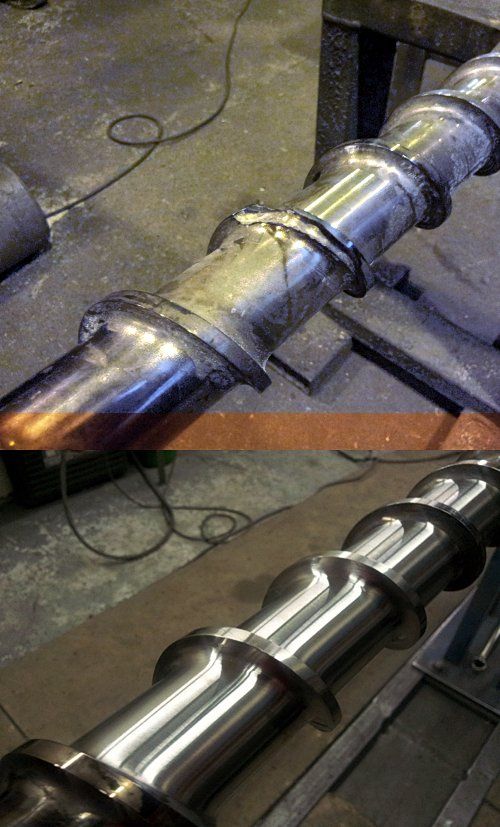
We’ve refurbished screws for more than 40 years. We rebuild worn extruder and injection moulding screws back to their original tolerances, and most screws can be refurbished several times. We hard-face the flights in Stellite 6, 12 or 1, or Colmonoy 56, and rebuild corrosion-resistant Hastelloy screws with C276 alloy. While the screw is with us, we can renew or add nitriding, hard chrome plating or a tungsten coating.
A standard single-flighted extruder screw goes through these steps. We clean and straighten it, then grind the flight tips to remove the wear. We repair damaged flights and root, then add a buttering layer where needed to stop the hard-facing cracking. We pre-heat the screw, weld it and let it cool slowly. Finally we straighten and grind it, polish it, coat it if required, grind it to the recommended clearance and inspect it.
Gallery


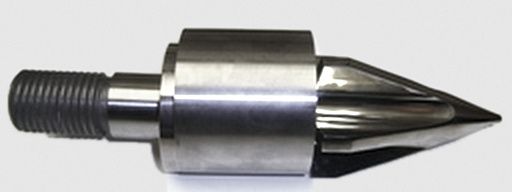
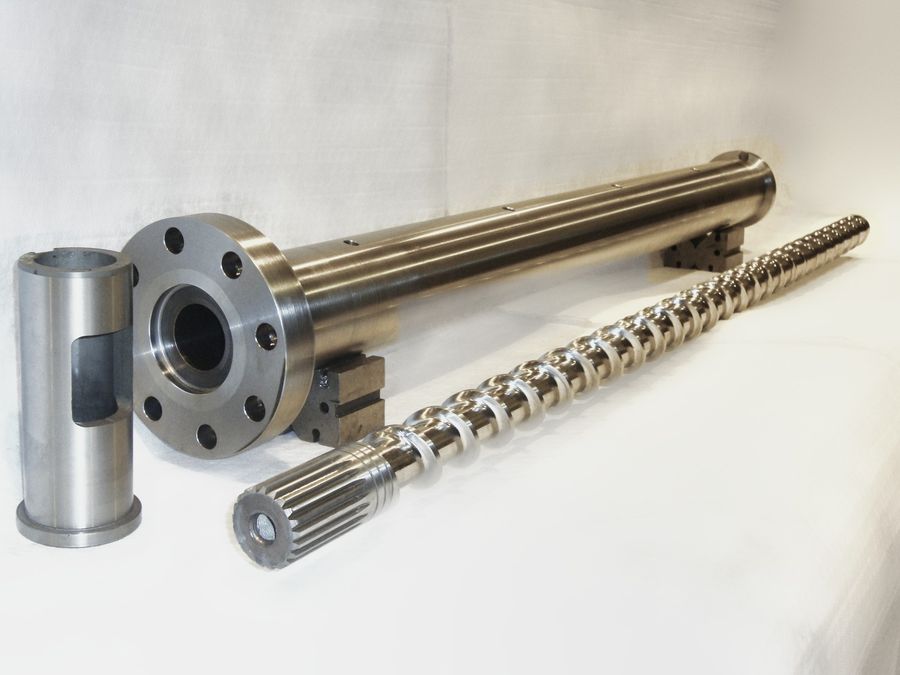
Why it matters
Once we’ve drawn your screw, the drawing stays on our database for the next job. When we manufacture you a new screw, we can refurbish the old one to as-new condition. That gives you a spare to run while the other is in for refurbishment.
Get in touch
Mon–Thu 07:30–16:15 · Fri 07:30–15:00
Need a new screw or a refurb quote? Call the workshop or send an enquiry — we’ll advise on the right route for your process.
Call +44 (0) 1706 655402 Send an enquiry